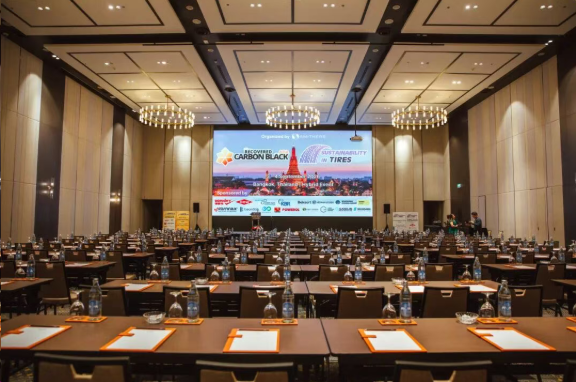
The global wave of waste tire recycling is surging forward. As a core pillar of the circular economy, recycled carbon black (rCB) is transforming from a by-product into a high-profile green material. Held in Bangkok, Thailand on September 3–4, 2026, the Asia Recycled Carbon Black Conference ran alongside the 2026 Tire Sustainability Conference. The event brought together decision-makers, technical experts and business leaders across the full global value chain of tires, pyrolysis and carbon black, to discuss technological upgrades, quality improvement and commercialization of the recycled carbon black sector.
Conference Theme & Key Highlights
The conference addressed common challenges facing the waste tire pyrolysis industry: inconsistent quality of recycled carbon black, incomplete industry standards, obvious shortcomings in post-treatment processes, and difficulties in high-value application deployment. It aimed to connect the full chain of “technology – quality standards – application – commercialization” and explore viable paths for large-scale industrial development.
Doright’s Highlight Presentation: Recycled Carbon Black Wet pelletizing System
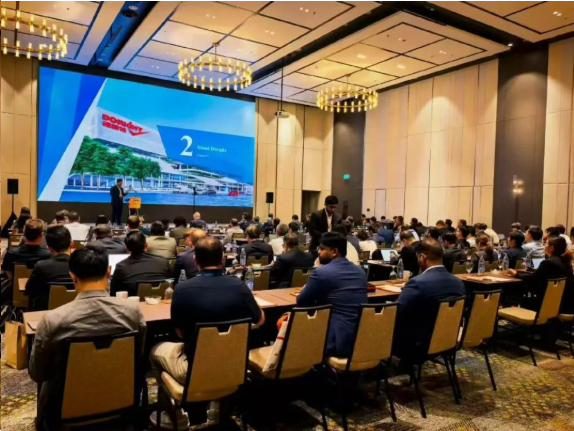
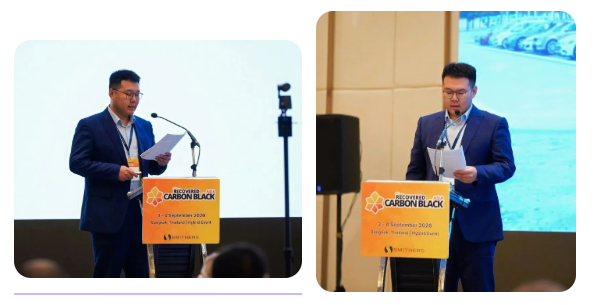
Custom-engineered, Proven & Reliable On the second day of the conference, Hu Yunchao, R&D Engineer of Doright, delivered a keynote speech titled Recycled Carbon Black Wet pelletizing System. He comprehensively introduced the company’s technical expertise and industrial application experience in complete post-treatment equipment for recycled carbon black.
The speech elaborated on Doright’s self-developed recycled carbon black wet pelletizing system. Matching production capacity planning, site operating conditions and process targets, the system allows flexible selection of capacity rating, drying methods and heating systems to precisely meet the practical requirements of various recycled carbon black manufacturers. In addition, the production line adopts a compact layout, greatly improving land utilization and effectively cutting civil engineering renovation costs, which solves the widespread problem of limited space for retrofitting old workshops.
The complete system consists of five core modules: powder conveying, wet pelletizing, drying, cooling, screening & impurity removal, and finished product storage & packaging. The whole process is controlled via DCS automation:
✔ Excellent pelletizing performance: particle roundness >0.7, finished product pass rate >85%;
✔ Fully sealed design with zero dust leakage for a clean and eco-friendly production environment;
✔ System heat loss <20%; pyrolysis gas and pyrolysis oil can be directly used as heat sources to reduce plant energy consumption;
✔ Low-NOₓ combustion system, NOₓ emission <150mg/m³, complying with environmental emission standards;
✔ Equipped with high-gradient electromagnetic iron removal device for efficient removal of weakly magnetic impurities to guarantee rCB finished quality;
✔ The full set of equipment has been long validated in multiple industrial projects, featuring mature technology, stable operation and reliable performance, with many completed projects at home and overseas.
Combined with key indicators including feed ash content, toluene transmittance and oil absorption value, the speech explained how raw material properties affect pelletizing processes and equipment selection, and shared pelletizing test data from our in-house laboratory, delivering practical engineering references for production line selection and process commissioning.
The presentation received enthusiastic feedback. Many attendees visited the Doright booth for in-depth exchanges. Doright secured numerous inquiries and quotation opportunities, and arranged multiple follow-up post-conference site visits.
Deeply Rooted in the Industrial Chain, Empowering Recycled Carbon Black with Equipment Technology
While the recycled carbon black industry is moving from concept to large-scale industrialization, it still faces many hurdles: unstable product quality, poor equipment adaptability, high energy consumption and difficult dust control. Faced with these challenges, Doright does not merely supply standalone equipment. Instead, we extend our business to upstream and downstream sectors, striving to deliver full-turnkey solutions covering tire shredding, pyrolysis, grinding, pelletizing, drying and packaging, helping customers boost the added value of recycled carbon black products.
Going forward, Doright will further reduce equipment energy consumption, improve particle quality and automation level. We will continue to increase R&D investment to develop new process equipment for modification and purification. Leveraging our in-house pelletizing laboratory, we provide value-added services including feedstock testing, customized equipment design and on-site technical guidance. We will strengthen collaboration with global industrial partners, including pyrolysis plants, tire manufacturers and research institutes, to advance recycled carbon black toward higher quality and broader application scenarios.